 TEL +86-13923172919
Tube vs Solid-State HF Welder: Retrofit Cost, Downtime, and Payback
A manufacturing plant running several 10KW to 15KW legacy vacuum-tube high-frequency (HF) welding machines for TPU inflatable products or heavy-duty PVC tarpaulins often hits a familiar operational wall: rising electricity bills, frequent unplanned downtime waiting for replacement oscillator tubes, and unstable weld seams whenever ambient factory temperatures or line voltages fluctuate.
When evaluating a tube HF welder retrofit to a modern solid-state RF generator, plant managers rarely need another abstract comparison of oscillator physics. What matters on the factory floor is clear: how much does the conversion cost, how long will the line sit idle during installation, what real energy and maintenance savings can be expected, and how quickly does the upgrade pay for itself?
Why Factories Evaluate Solid-State HF Welding Upgrades
Traditional vacuum-tube HF welders have powered industrial plastic welding for decades because their mechanical frames and hydraulic or pneumatic presses are built to last. However, the high-voltage oscillator section inside older machines introduces recurring operational costs:
- Consumable Oscillator Tubes: Industrial vacuum tubes degrade over operating hours. Replacing a high-power oscillator tube is expensive, and unexpected tube failure halts production until a spare arrives and is re-tuned.
- High Thermal Loss and Energy Waste: Vacuum-tube generators typically convert only 50% to 60% of input electrical power into usable radio-frequency (RF) welding energy. The rest dissipates as waste heat, driving up factory electricity consumption and straining cooling systems.
- Warm-Up Delay and Parameter Drift: Tube filaments require warm-up time before reaching stable output. Across a multi-shift day, thermal drift can cause inconsistent weld penetration, forcing operators to manually adjust tuning capacitors or welding timers.
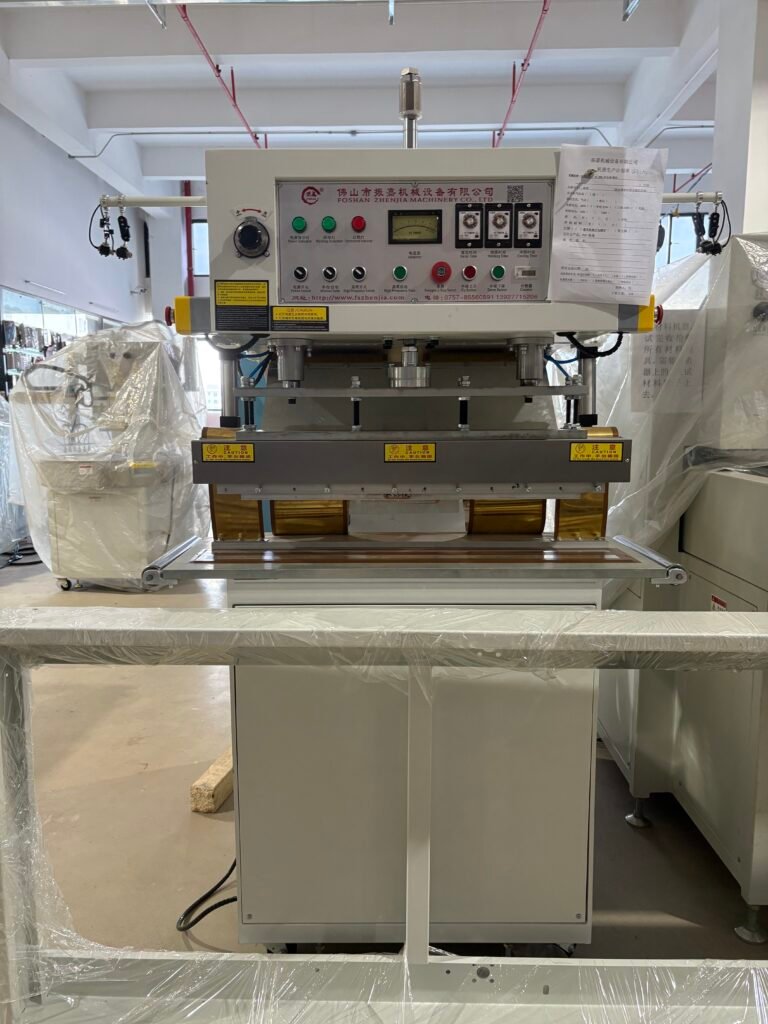
A solid state HF welding upgrade replaces the high-voltage transformer, rectifier stack, and vacuum tube assembly with transistorized (MOSFET/LDMOS) RF power modules and digital PLC impedance matching—while retaining your existing mechanical press frame, pneumatic or hydraulic cylinders, and custom welding molds.
Retrofit vs. Full Machine Replacement: Capital Cost Reality
Before committing to an RF welder conversion, compare the total capital outlay against purchasing a brand-new solid-state HF welding machine.
| Evaluation Factor | Solid-State Generator Retrofit | Brand-New Solid-State HF Machine |
| Upfront Equipment Cost | Lower (reuses existing press frame, cylinders, and worktable) | Higher (full mechanical, hydraulic/pneumatic, and electrical build) |
| Tooling & Mold Compatibility | Uses existing upper electrodes, lower platens, and fixtures | Existing molds usually fit if platen dimensions and stroke match |
| Installation Downtime | 2 to 5 days per machine (disassembly, wiring, impedance tuning) | Minimal line disruption if installed alongside existing line |
| Mechanical Lifespan | Dependent on condition of existing press guides and cylinders | Full new mechanical and electrical service life |
When a retrofit makes financial sense:
- The existing press frame, guide pillars, and hydraulic or pneumatic system are structurally sound and maintain accurate platen parallelism.
- You operate specialized heavy-duty presses (such as large push-plate or multi-station rotary frames) where replacing the entire mechanical structure would require major rigging and floor modifications.
When a new machine is the better choice:
- The existing press suffers from worn guide bushings, leaking hydraulic cylinders, or an outdated mechanical frame that cannot hold consistent clamping pressure across the welding die. Upgrading the RF generator will not fix uneven mechanical pressure.
Installation Downtime and Engineering Scope
A successful HF generator replacement is not a simple plug-and-play swap. Because high-frequency energy at 27.12 MHz interacts directly with the mechanical geometry of your press and welding mold, proper integration requires structured engineering steps:
- Pre-Retrofit Inspection & Power Check: Confirming your factory electrical supply (e.g., 380V / 3-Phase / 50Hz or local plant voltage) and inspecting the condition of the upper electrode platen, insulation boards, and ground straps.
- High-Voltage Removal & Cabinet Mounting: Stripping out the old high-voltage oil or dry transformer, vacuum tube cavity, and mechanical variable capacitors, then mounting the compact solid-state RF power unit and matching box.
- Coaxial Feed & Grounding Optimization: Solid-state RF modules require low-inductance copper ground return paths and shielded coaxial connections to the upper electrode to prevent reflected power loss.
- Control Integration & Sample Proofing: Connecting the solid-state generator’s digital control interface to the machine’s PLC or timer relay, followed by sample testing on your actual PVC, TPU, or EVA materials to establish baseline power and cycle settings.
In a well-prepared factory, mechanical and electrical installation typically takes 2 to 4 working days per machine, plus 1 day for impedance matching and sample proofing with production tooling.
Operational Savings and Payback Drivers
Calculating the payback period for a solid-state conversion relies on three measurable operational factors rather than theoretical lab numbers:
1. Direct Electrical Energy Reduction
Solid-state RF generators typically achieve 75% to 85% electrical-to-RF conversion efficiency, compared to 50%–60% for legacy vacuum-tube units. Furthermore, solid-state systems draw minimal standby power between weld cycles because there is no continuous filament heating requirement. In factories running two shifts per day on high-power equipment (10KW and above), reduced kilowatt-hour draw directly lowers monthly utility overhead.
2. Elimination of Vacuum Tube & High-Voltage Component Replacements
Over a 3-to-5-year production window, avoiding recurring purchases of replacement oscillator tubes, high-voltage rectifier diodes, and cooling blower assemblies eliminates a major line item from the maintenance budget.
3. Scrap Reduction and Faster Cycle Setup
Because solid-state generators use automatic digital impedance matching, power delivery remains consistent from the first weld of the morning shift to the last weld of the night shift. Operators spend less time compensating for power drift, reducing burnt edges, cold welds, and rejected inflatable or packaging units.
Note on Payback Period: Facilities running single-shift intermittent production with low-power machines (4KW–5KW) will see a longer payback horizon. Conversely, plants operating 8KW to 15KW+ machines across 16 to 24 hours daily on demanding materials like thick TPU or coated fabrics typically recover retrofit costs substantially faster through combined electricity, spare-part, and scrap savings.
Critical Technical & Safety Boundaries During Conversion
Modifying high-frequency industrial equipment carries strict electrical and mechanical boundaries that must never be overlooked:
- MUST verify full electrical isolation and discharge all high-voltage capacitors before opening or dismantling legacy vacuum-tube cabinets. Legacy transformers operate at lethal multi-kilovolt potentials.
- MUST maintain continuous, low-impedance copper grounding between the solid-state matching box, upper press head, and lower worktable. Improper grounding causes stray RF radiation, electronic control interference, and reflected power damage to solid-state output transistors.
- PROHIBITED: Never operate a retrofitted HF welder with shielding panels removed or cabinet safety interlocks bypassed. Even though solid-state units eliminate multi-kilovolt tube anode plates, high-frequency electromagnetic energy at the electrode still causes severe deep-tissue RF burns upon contact.
- NEVER run the solid-state generator into an open circuit or an unmatched welding mold without verifying reflected power limits. While modern solid-state generators include built-in VSWR (Voltage Standing Wave Ratio) protection and fast electronic arc suppression, incorrect electrode insulation or damaged buffer sheets will still trigger fault shutdowns or damage custom brass molds.
Checklist Before Requesting a Retrofit Assessment
If you are considering converting existing tube-based HF welders in your plant, prepare the following details before consulting an equipment engineer:
- Current Machine Nameplate & Power Rating: Rated kW output, operating frequency (confirming 27.12 MHz), and press type (C-frame, push-plate, oil-pressure, or rotary table).
- Factory Power Supply: Available voltage, phase, and frequency at the machine disconnect switch.
- Platen & Mold Dimensions: Maximum upper electrode plate size and the surface area of your largest welding die.
- Primary Materials & Thickness: Specific thermoplastics welded (e.g., PVC, TPU, PU-coated fabric, EVA) and total layer thickness.
- Daily Operating Hours: Number of shifts per day and average welds per hour to calculate realistic energy and maintenance ROI.